

We bring 40 years of proven engineering solutions to the world’s demanding, compliance-regulated industries — Expertise that your plan can rely on.
From pharmaceutical majors to global FMCG brands, our systems operate in process facilities where water quality is maintained with zero margin for impurity error.
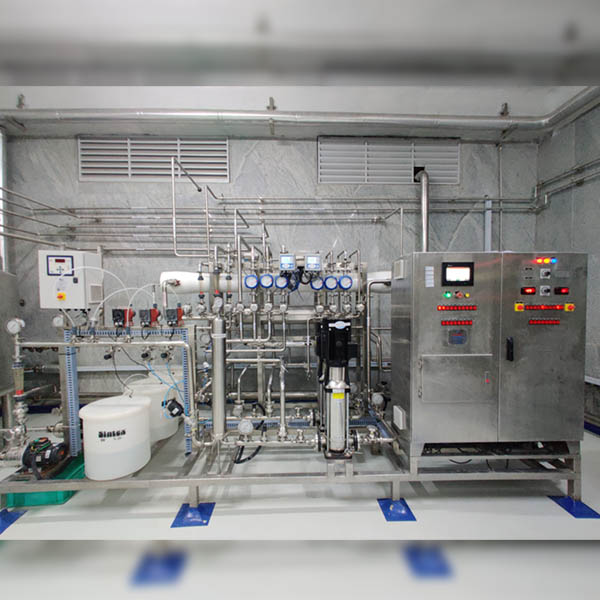
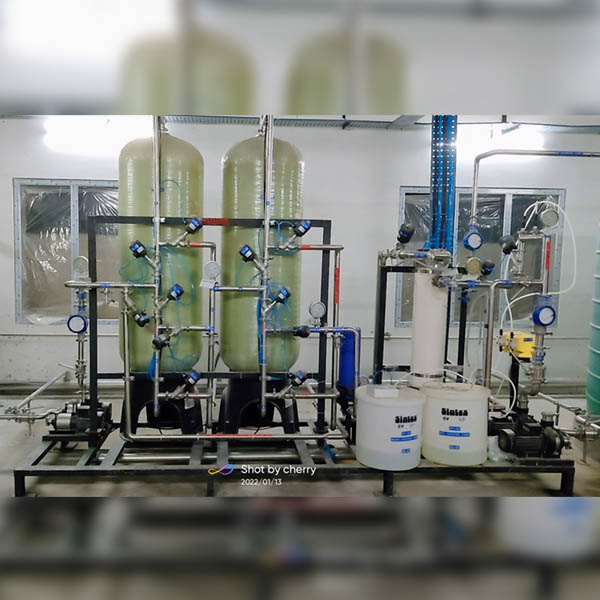
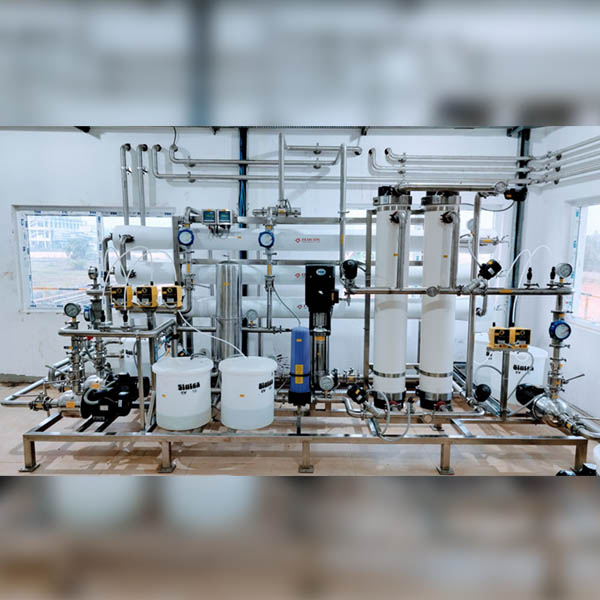
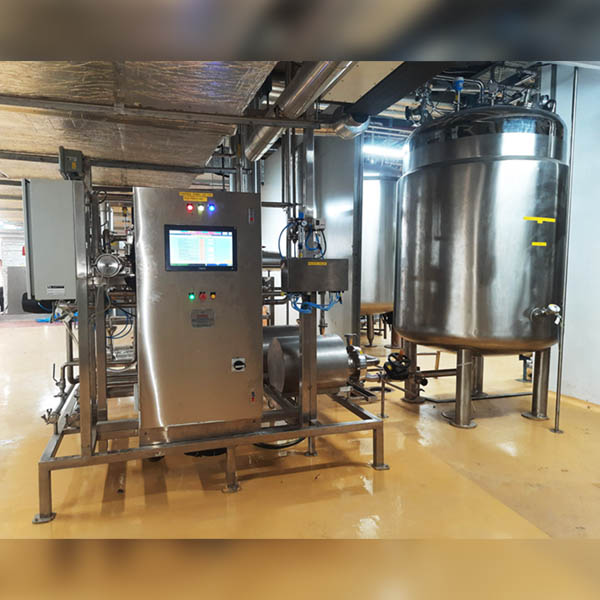
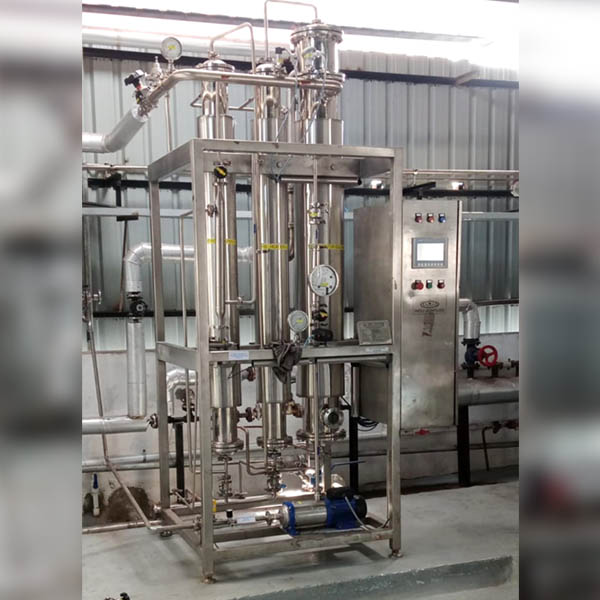
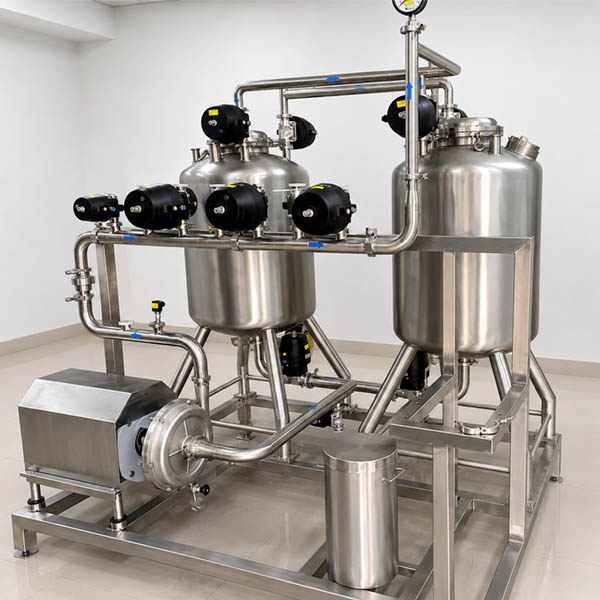
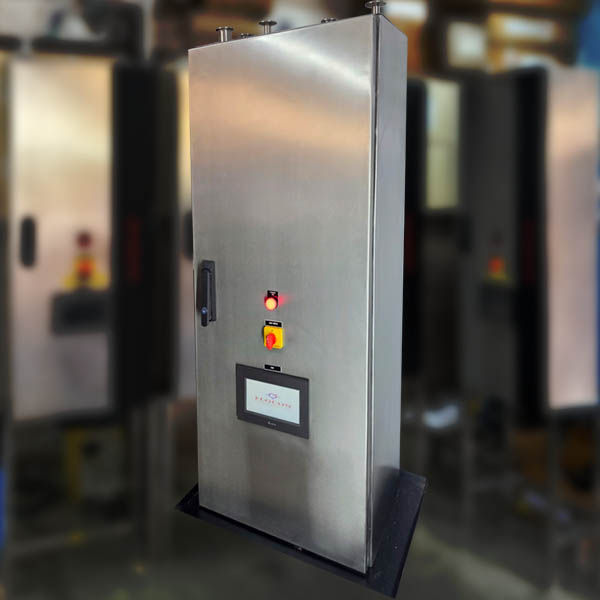
From pretreatment to WFI, pure steam to automation — We are your dependable partner across the entire system lifecycle for systems, equipments and after sales service.
Our systems are designed audit-ready in accordance with standard regulations and validated against FDA, EU GMP, and WHO guidelines, with full DQ/IQ/OQ documentation support.
We understand that operational factors vary from plant to plant. Thus we provide a bespoke system that is designed around your feed water, layout, and production targets.
We understand that operational factors vary from plant to plant. Thus we provide a bespoke system that is designed around your feed water, layout, and production targets.
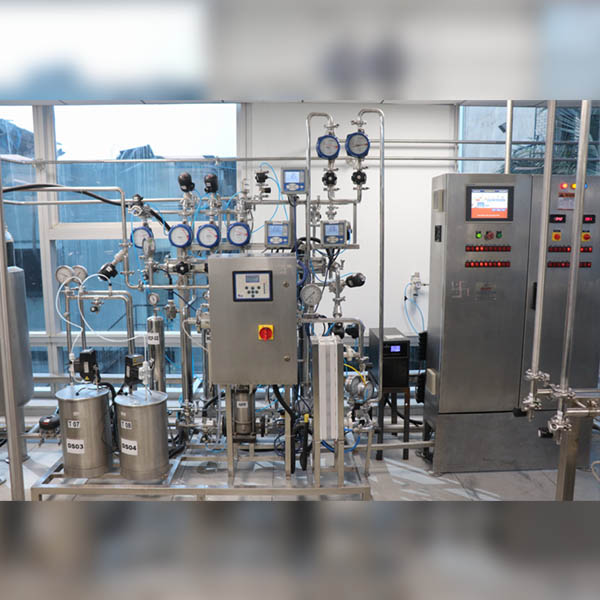
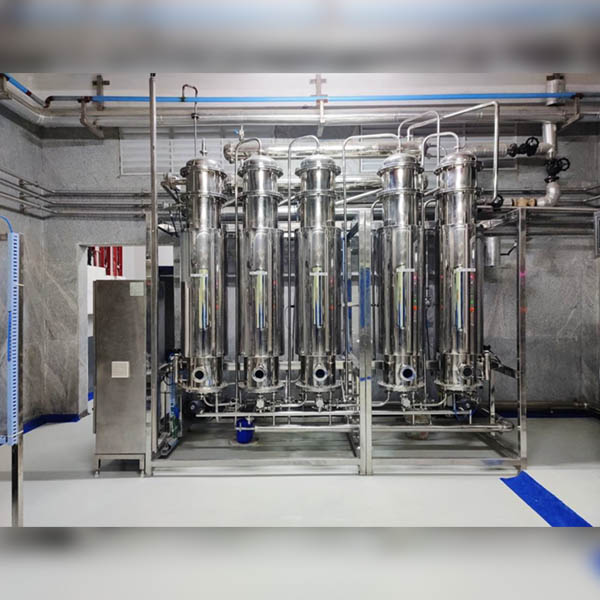
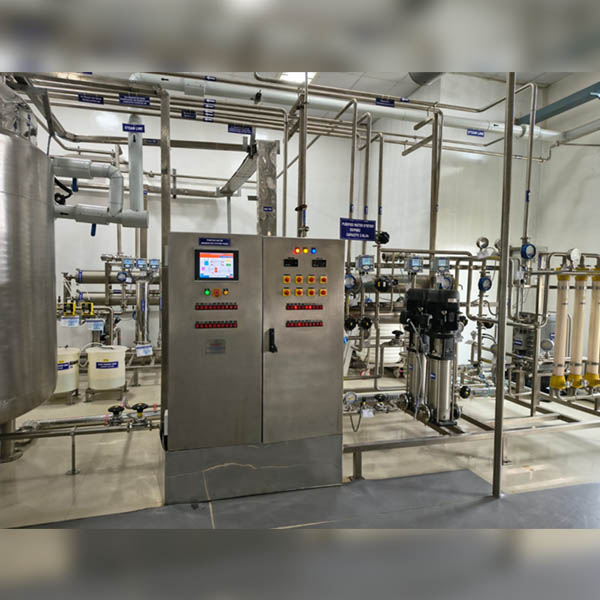
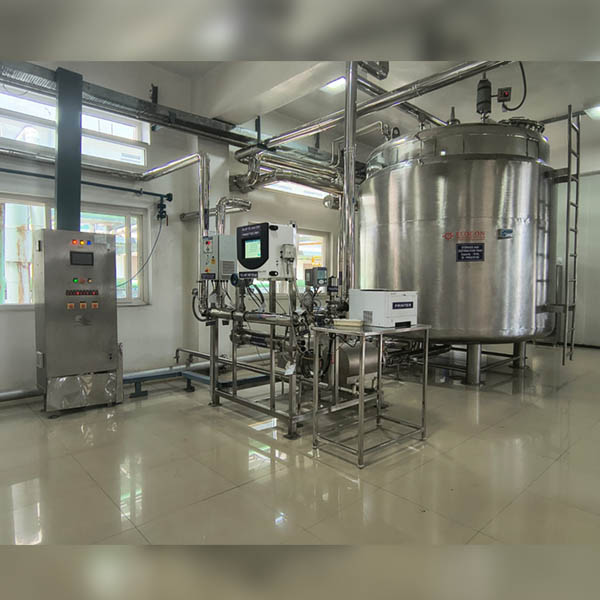

"Flocon Industries completely transformed our operational efficiency! We used to waste precious water and significant amounts of steam caused by flushing the system manually; Flocon solved this completely. By strategically implementing steam traps at every single user point, they eliminated manual flushing entirely. From their brilliant initial evaluation to flawless implementation, they saved us an incredible amount of time and energy. If you need pharma water system solutions, Flocon is the absolute best!"
Our association with Flocon is defined by three key pillars: Unmatched Reliability: Flocon’s systems have consistently met the rigorous regulatory standards required for our global operations, ensuring seamless uptime and product integrity. Technical Excellence: The depth of engineering expertise within the Flocon team has provided us with customized solutions that address our most complex water-handling challenges. Shared Values: Beyond the hardware, it is the transparency and responsiveness of the Flocon team that makes them a preferred partner. They operate with a customer-first mindset that aligns perfectly with MSN’s own dedication to excellence.

FLOCON Industries has been a trusted and reliable partner in supporting our operations with high-quality water systems and engineering solutions. Their strong technical knowledge, expertise, consistency of product performance, and customer-focused approach have added significant value to our manufacturing processes over the years. What stands out most of all is their commitment to quality, responsiveness, and ability to understand evolving operational needs, ensuring seamless integration and long-term reliability. Our continued association with FLOCON Industries is a reflection of confidence and trust they have built through their professionalism and service excellence.
"Flocon Industries is one of the most trusted suppliers to Natco Pharma Ltd. Their team demonstrated deep knowledge of pharmaceutical process requirements, especially in PW Generation, PW and WFI Storage & distribution systems. We are satisfied with the overall project outcome."
With reference to the work carried out at our plant, we appreciate the professionalism and technical understanding shown by the Flocon team. Your team completed the project within committed timelines. Flocon Industries consistently maintained high safety and quality standards at our manufacturing site. The speed and workmanship exceeded our expectations.